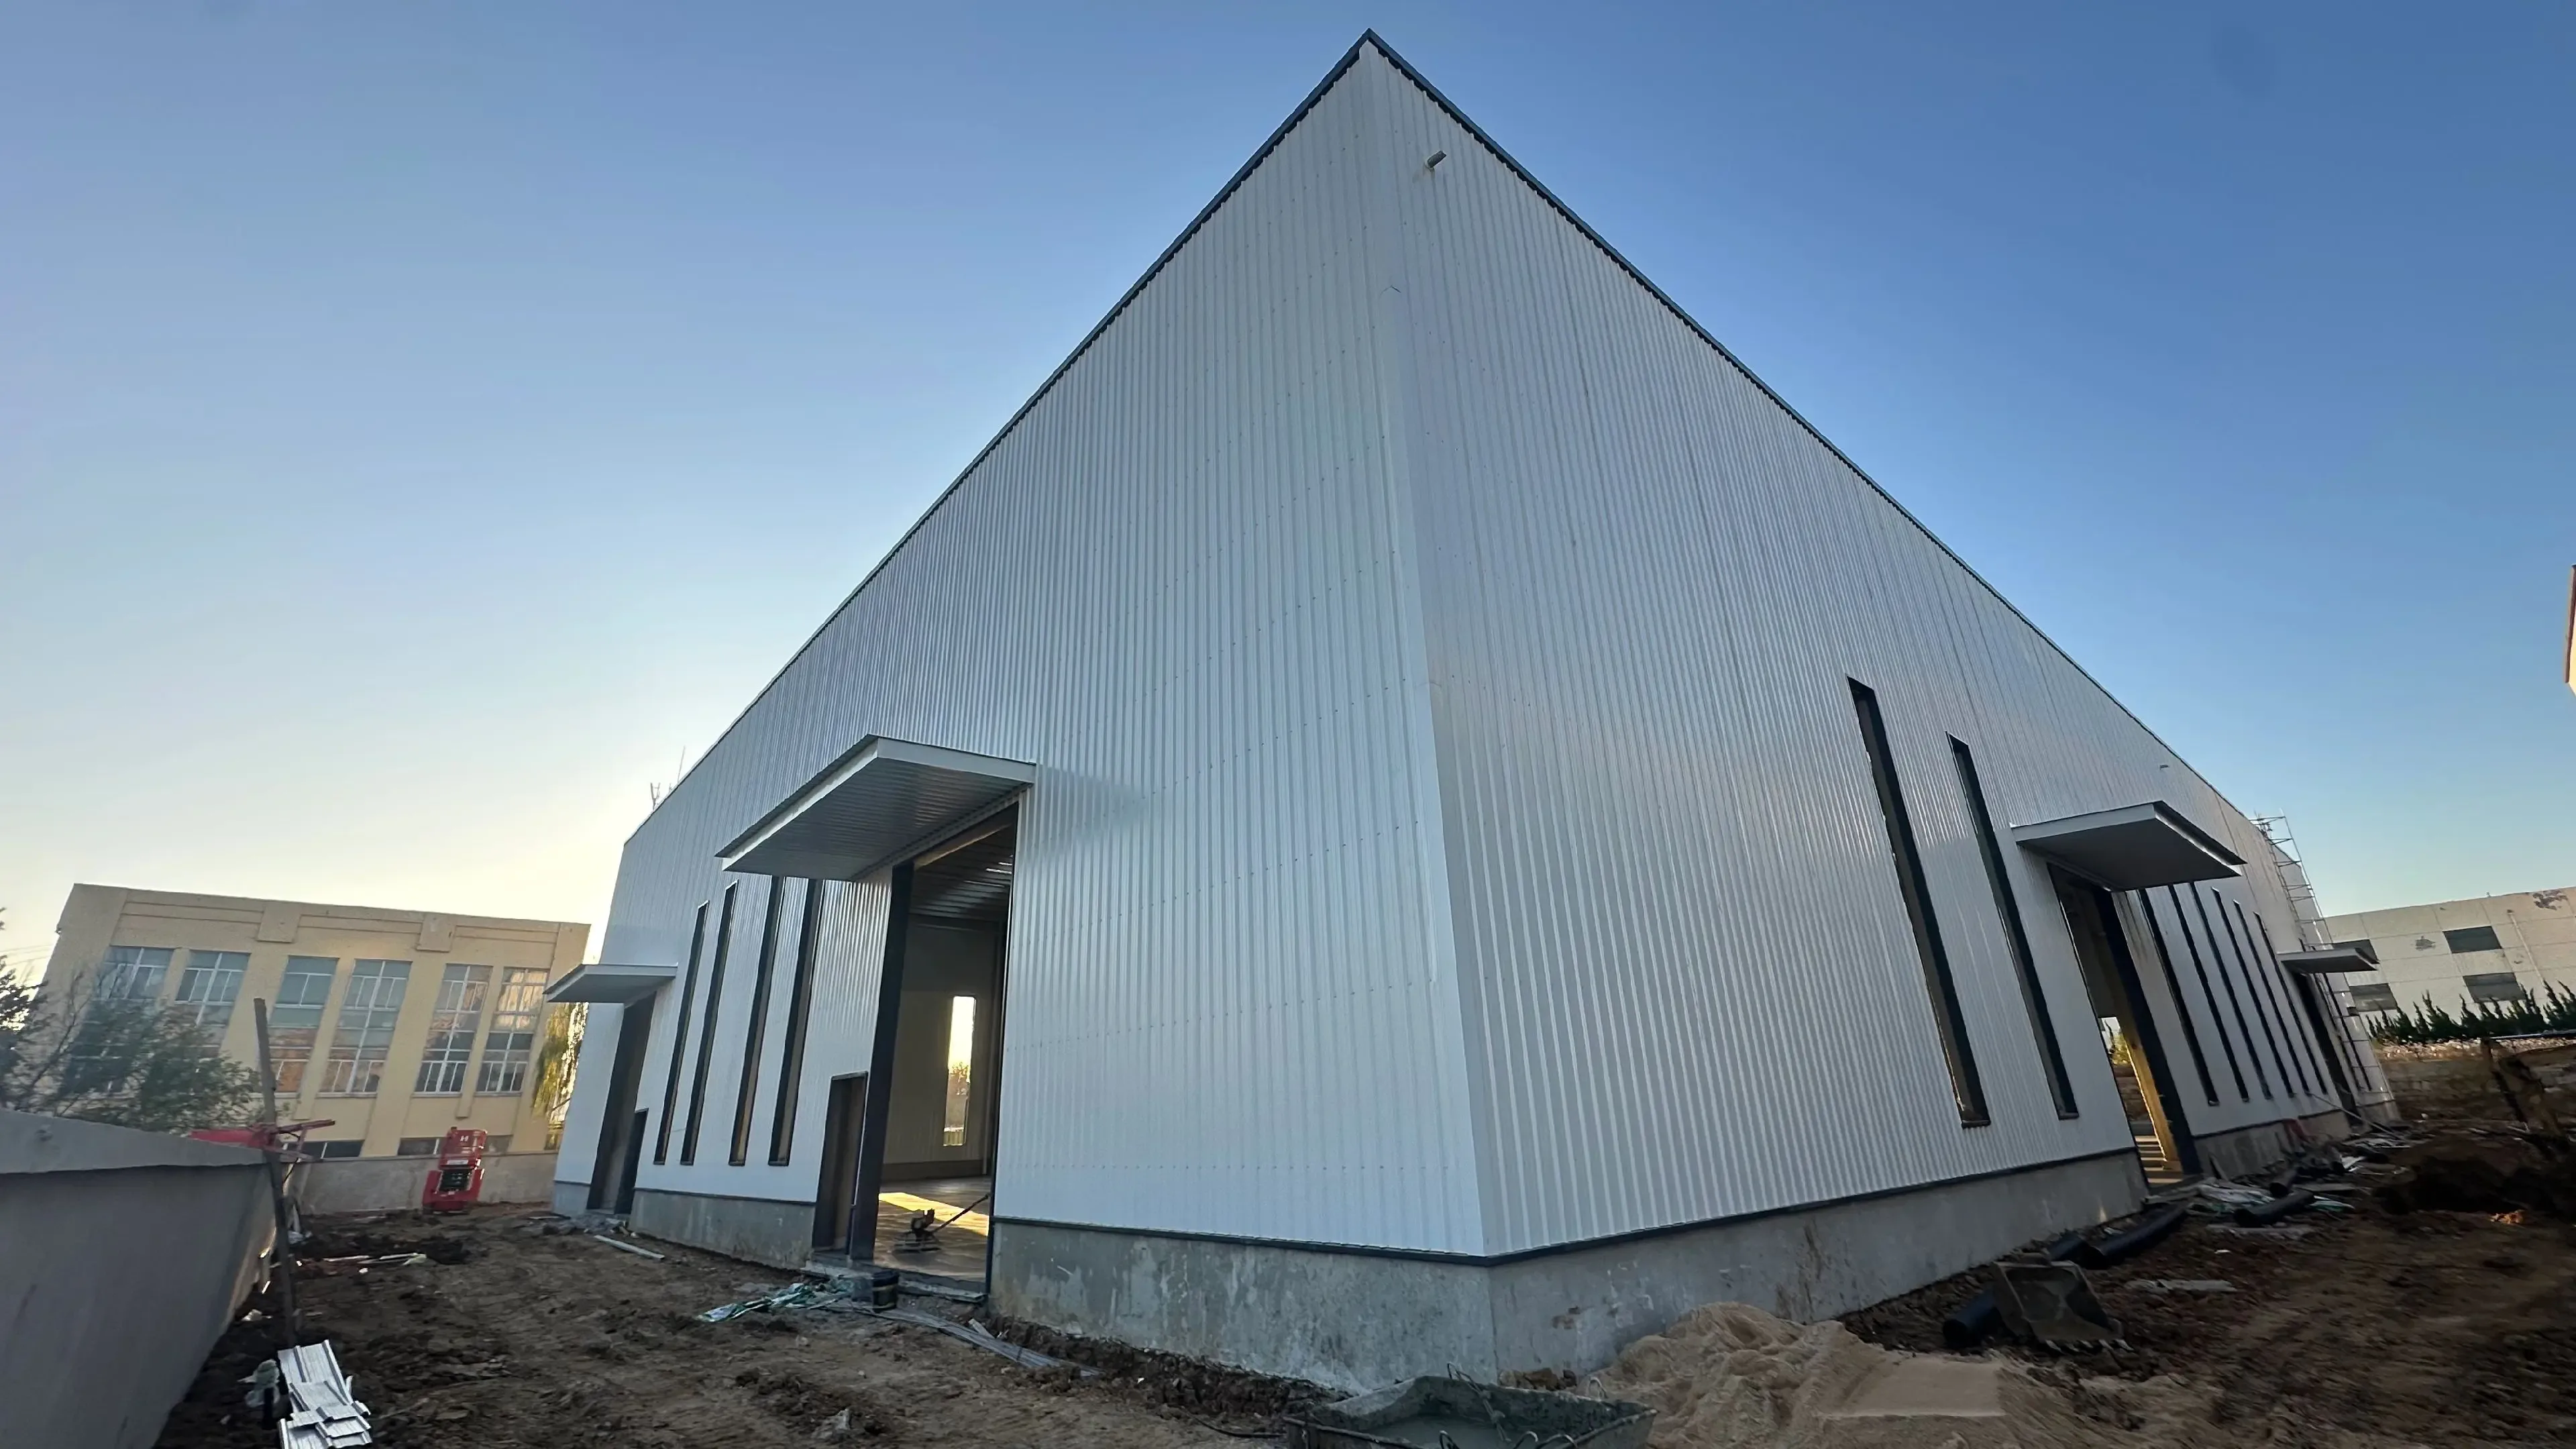
01 · Prefabricated Steel Structure Warehouse: Project Overview and Delivery Objective
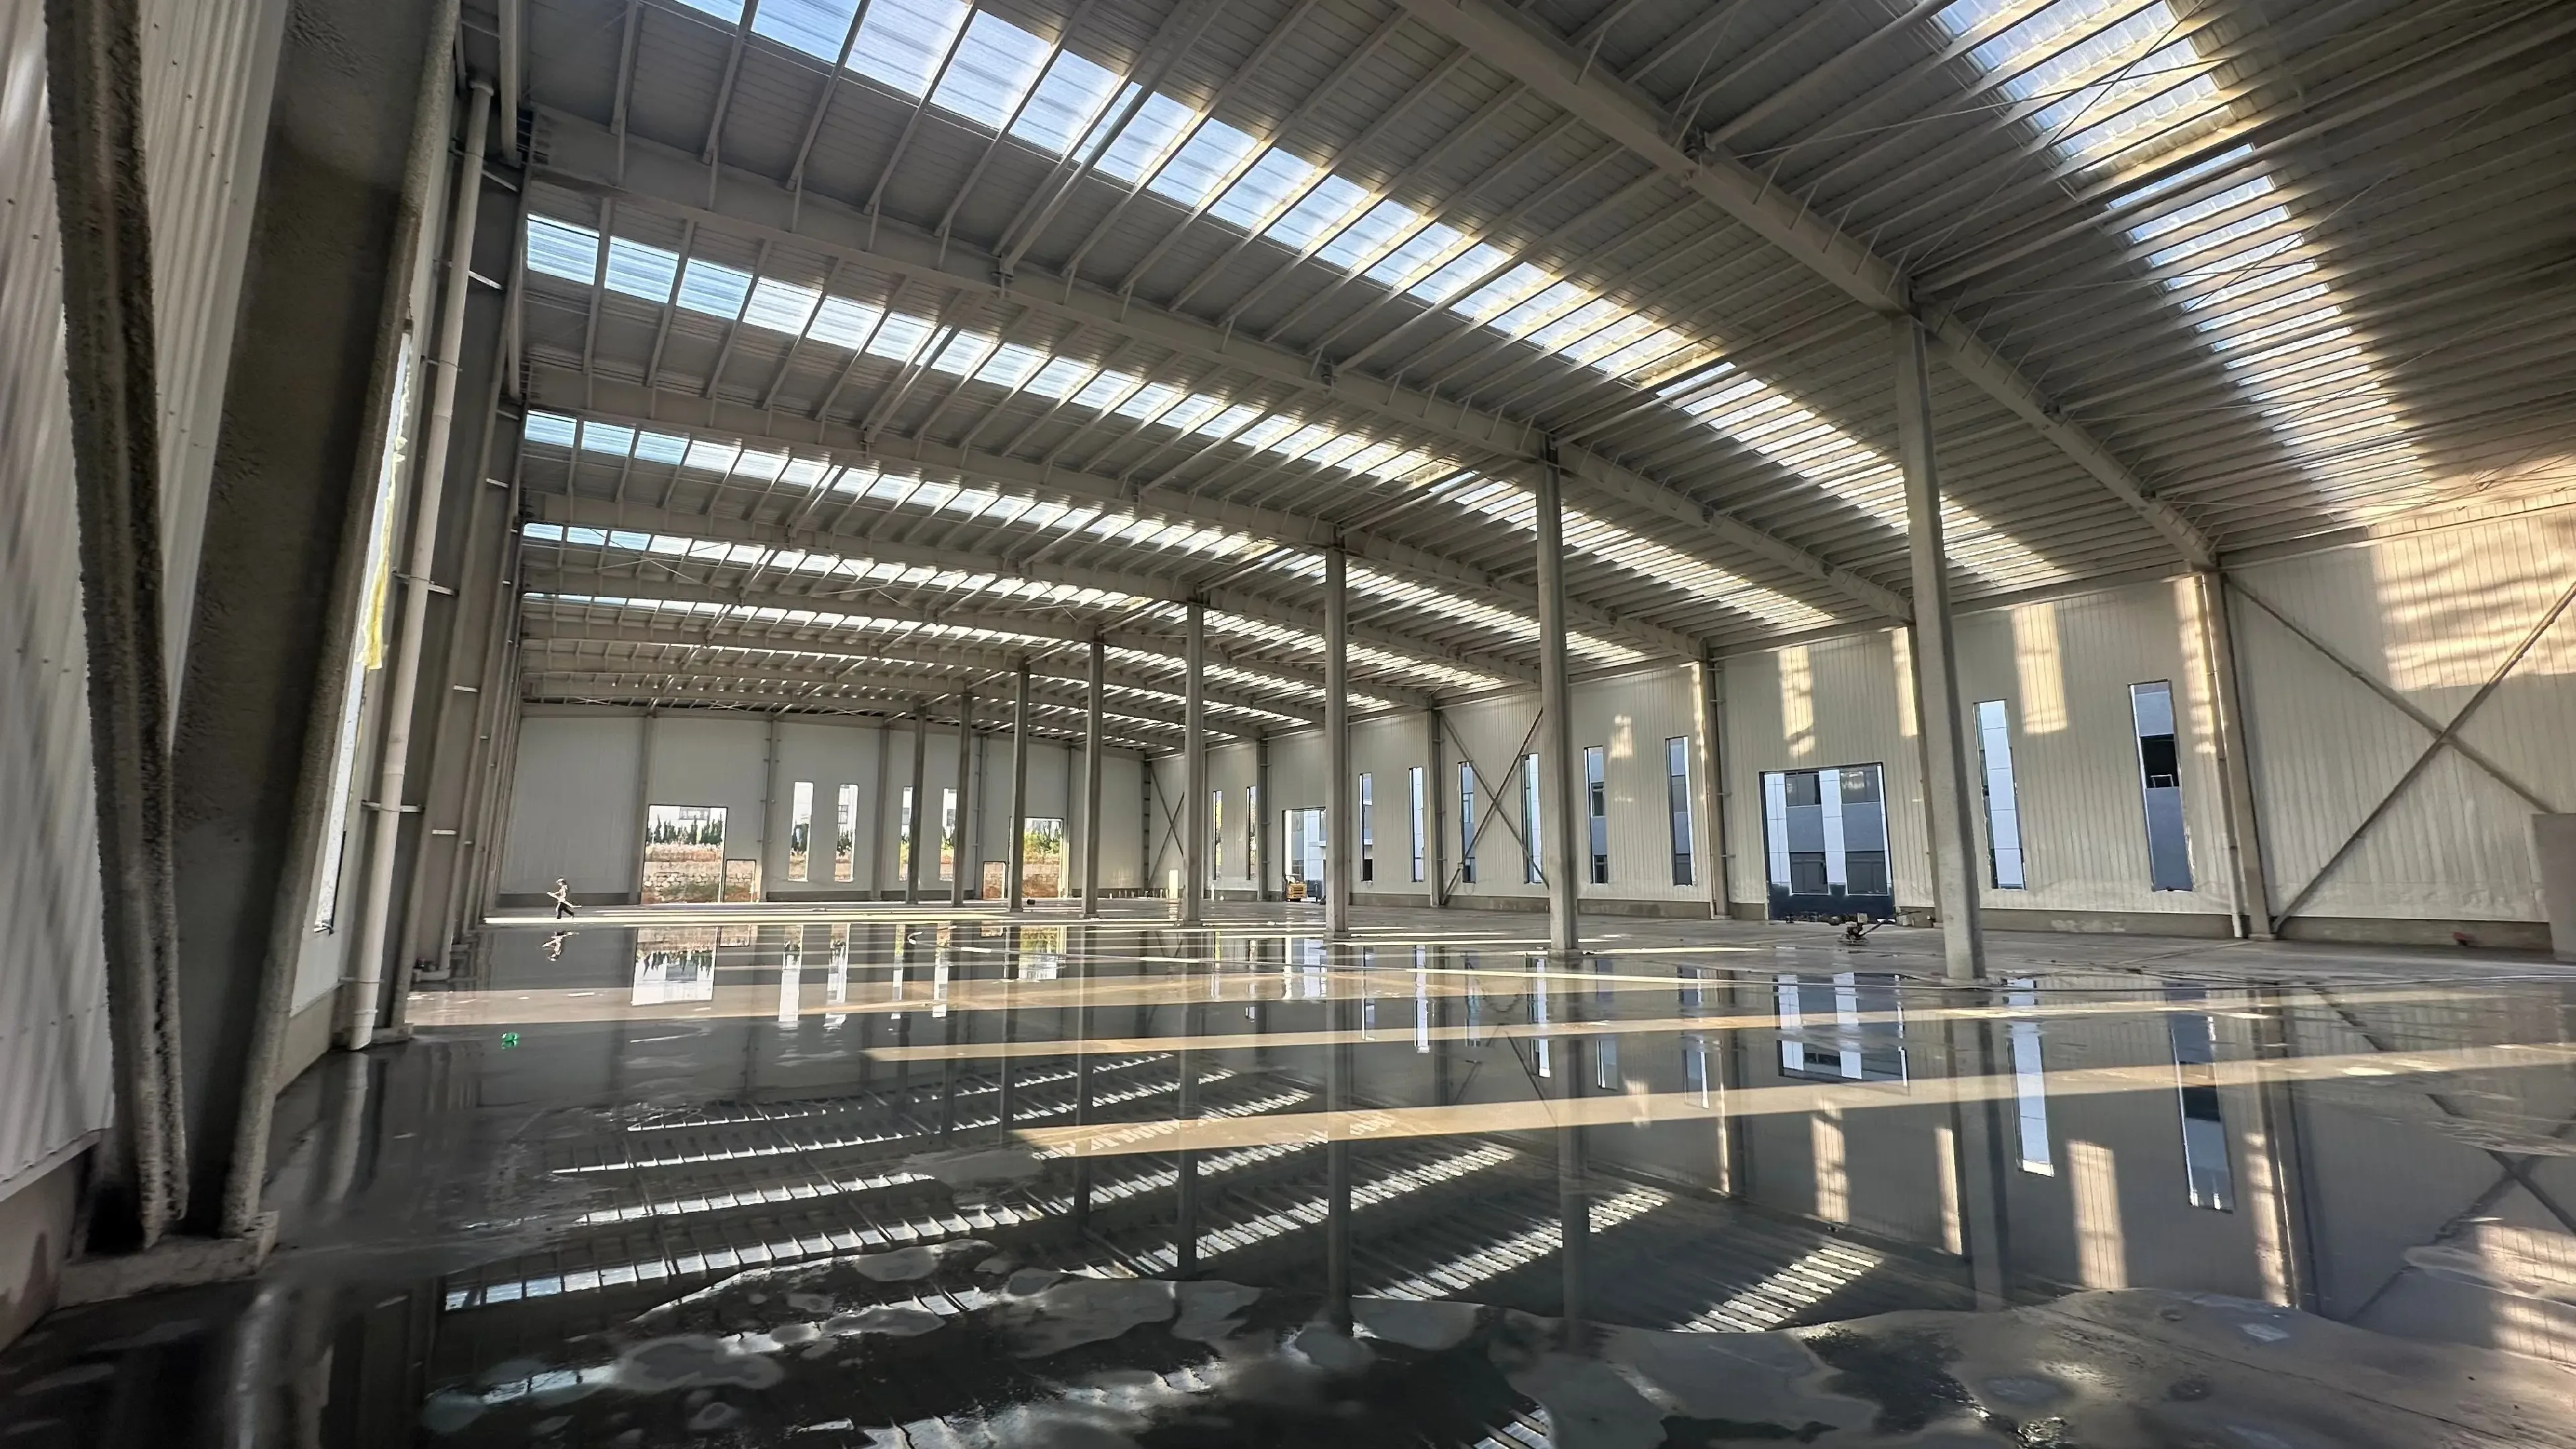
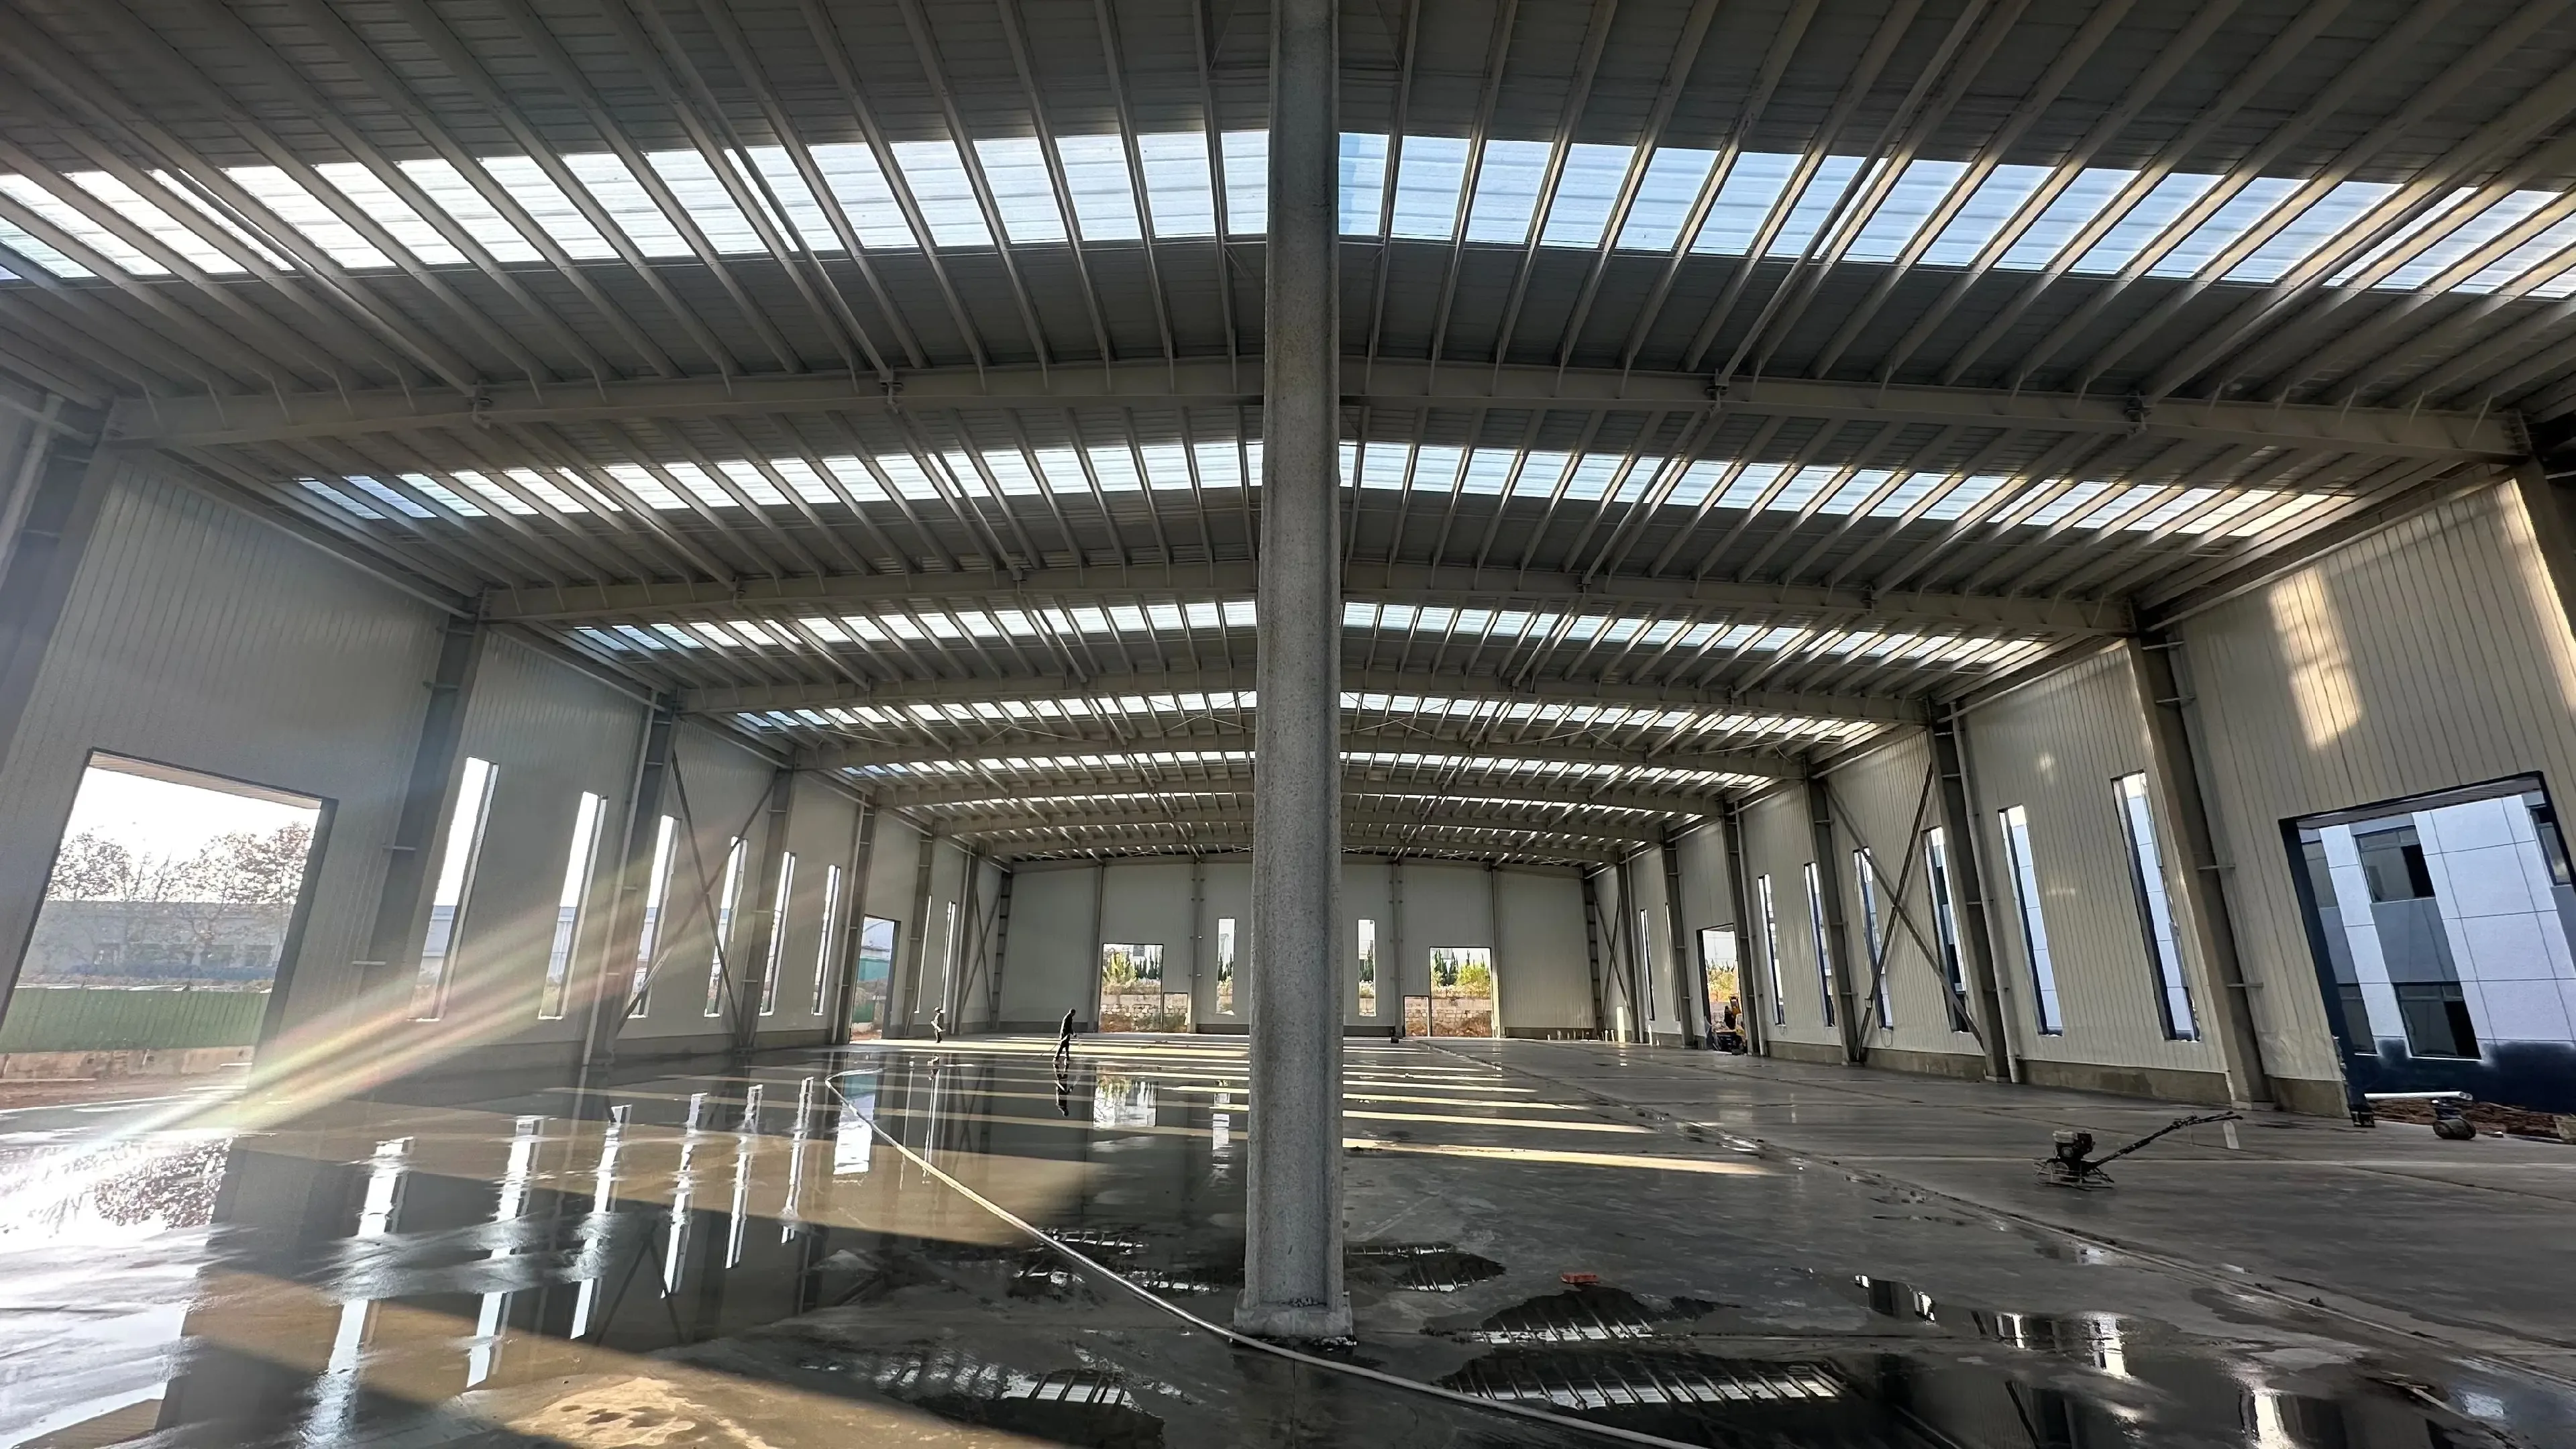
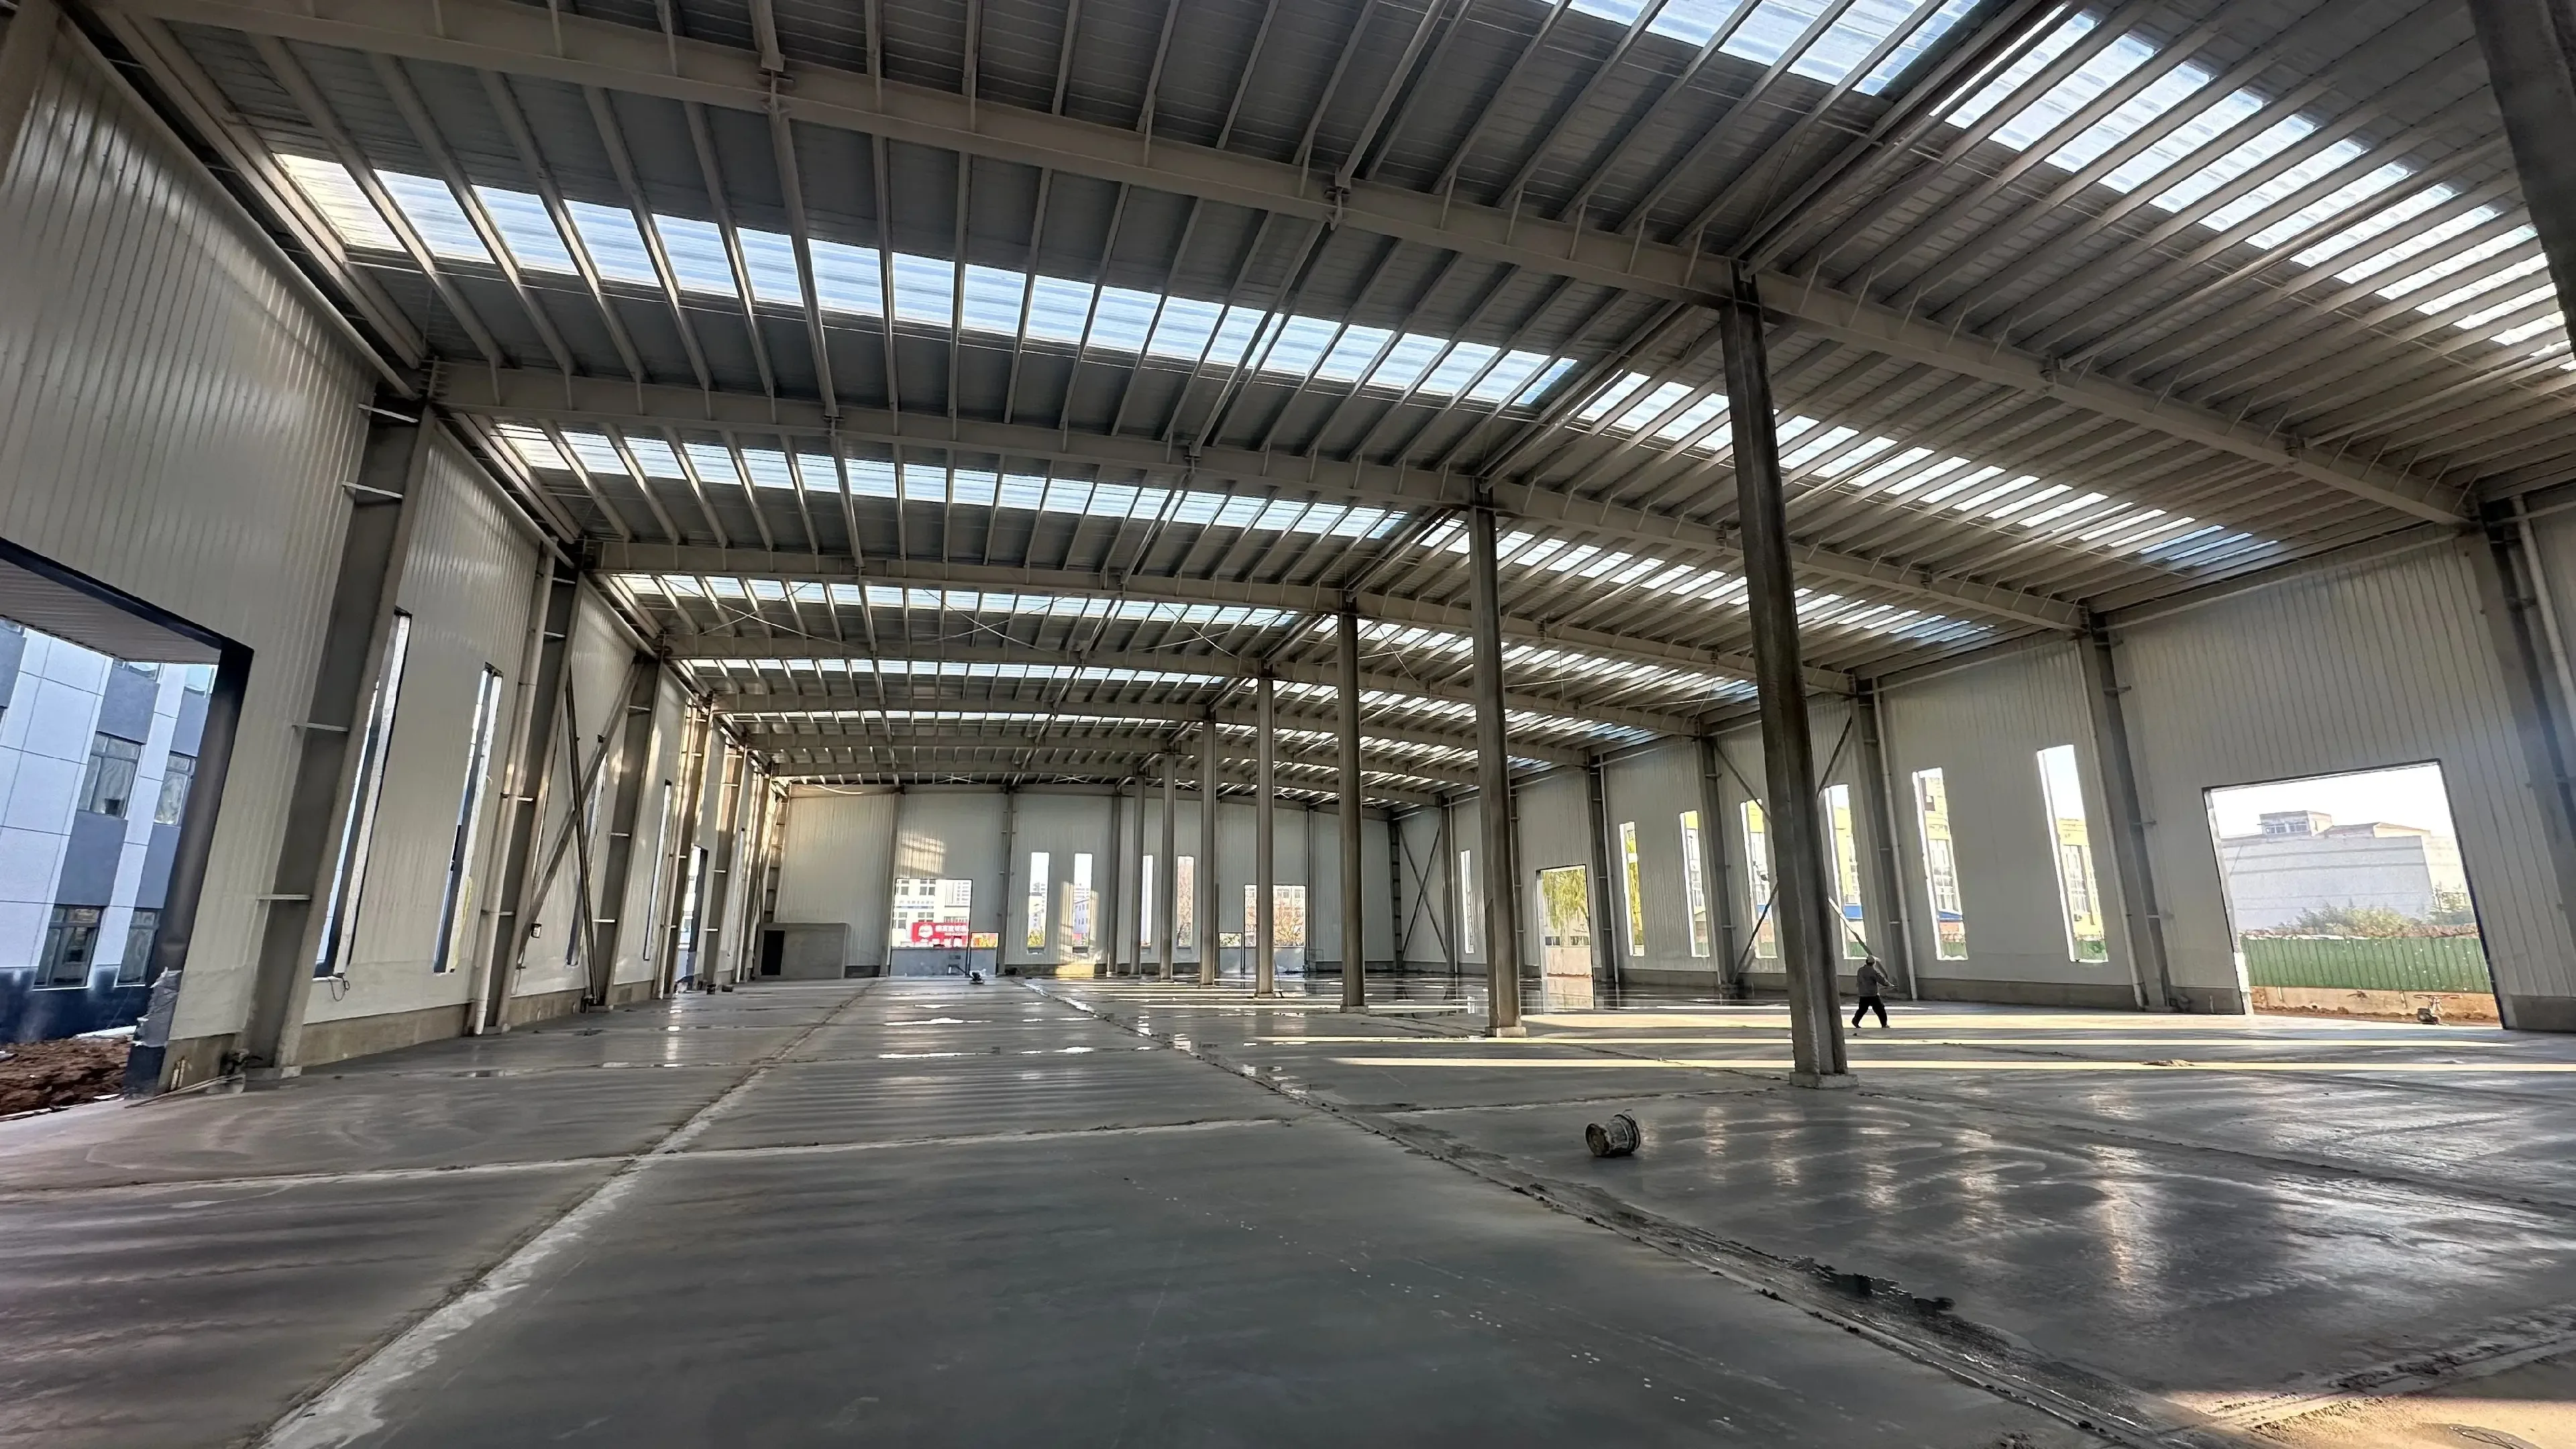
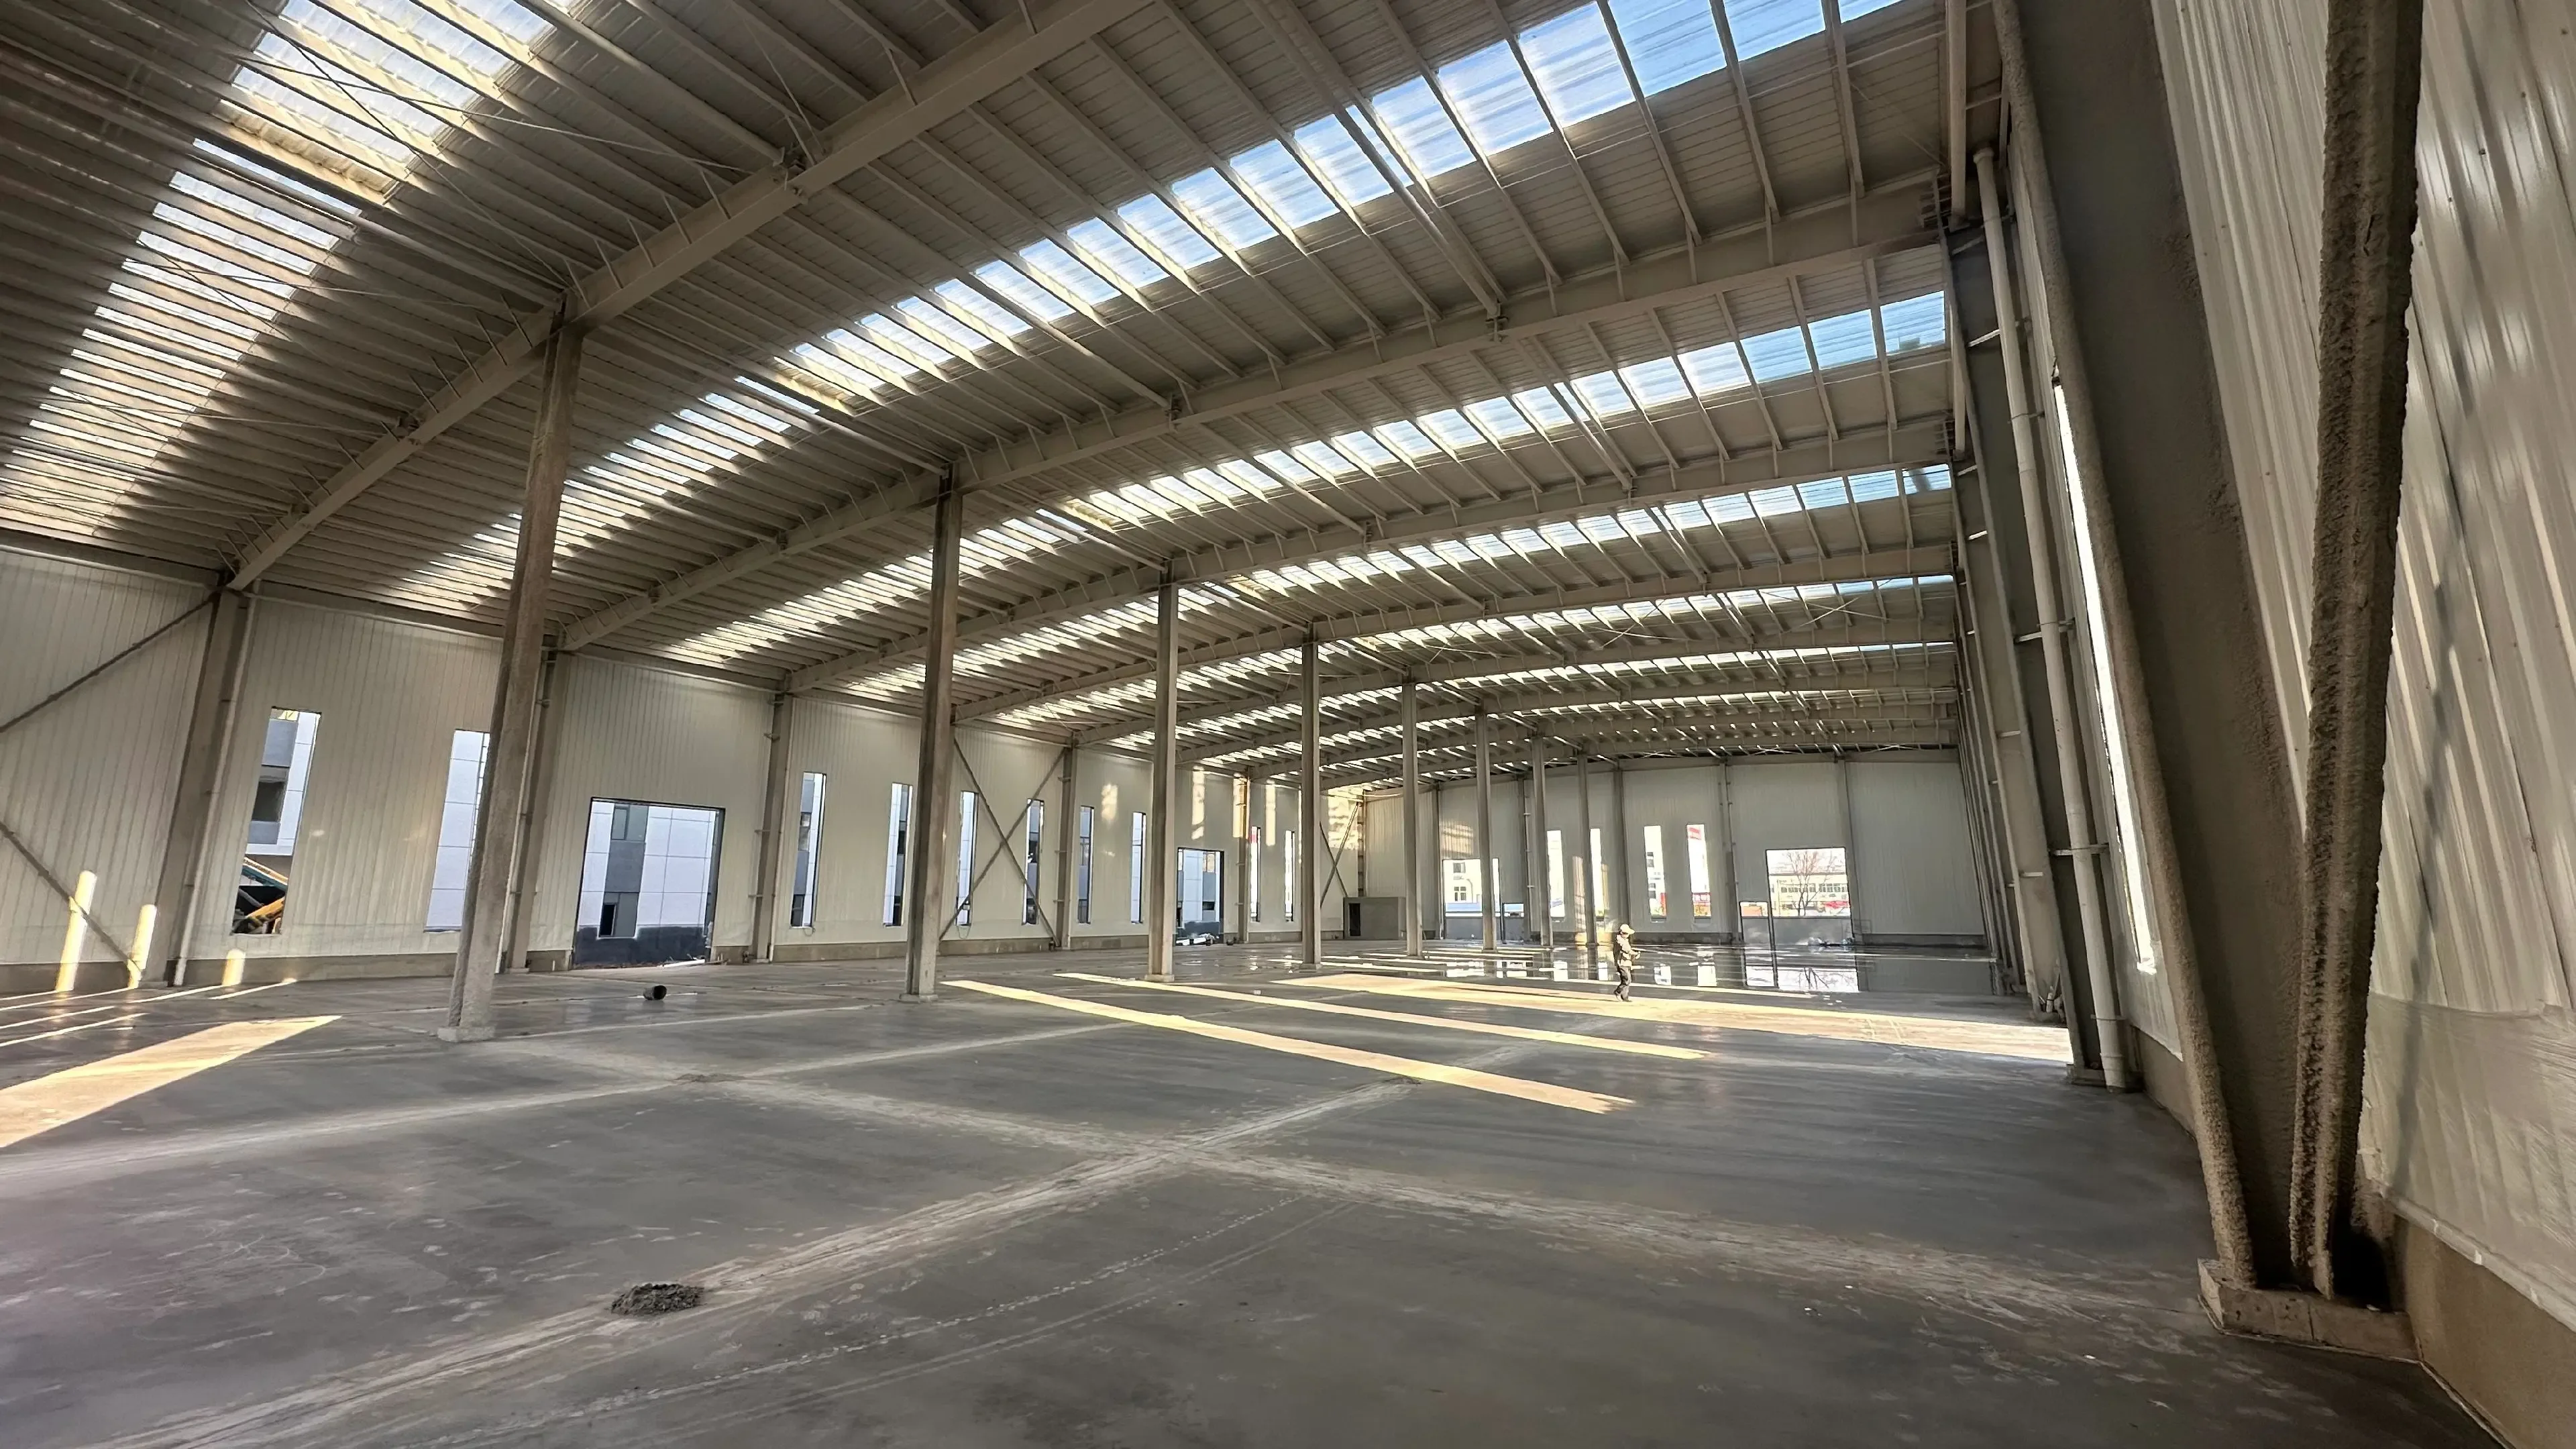
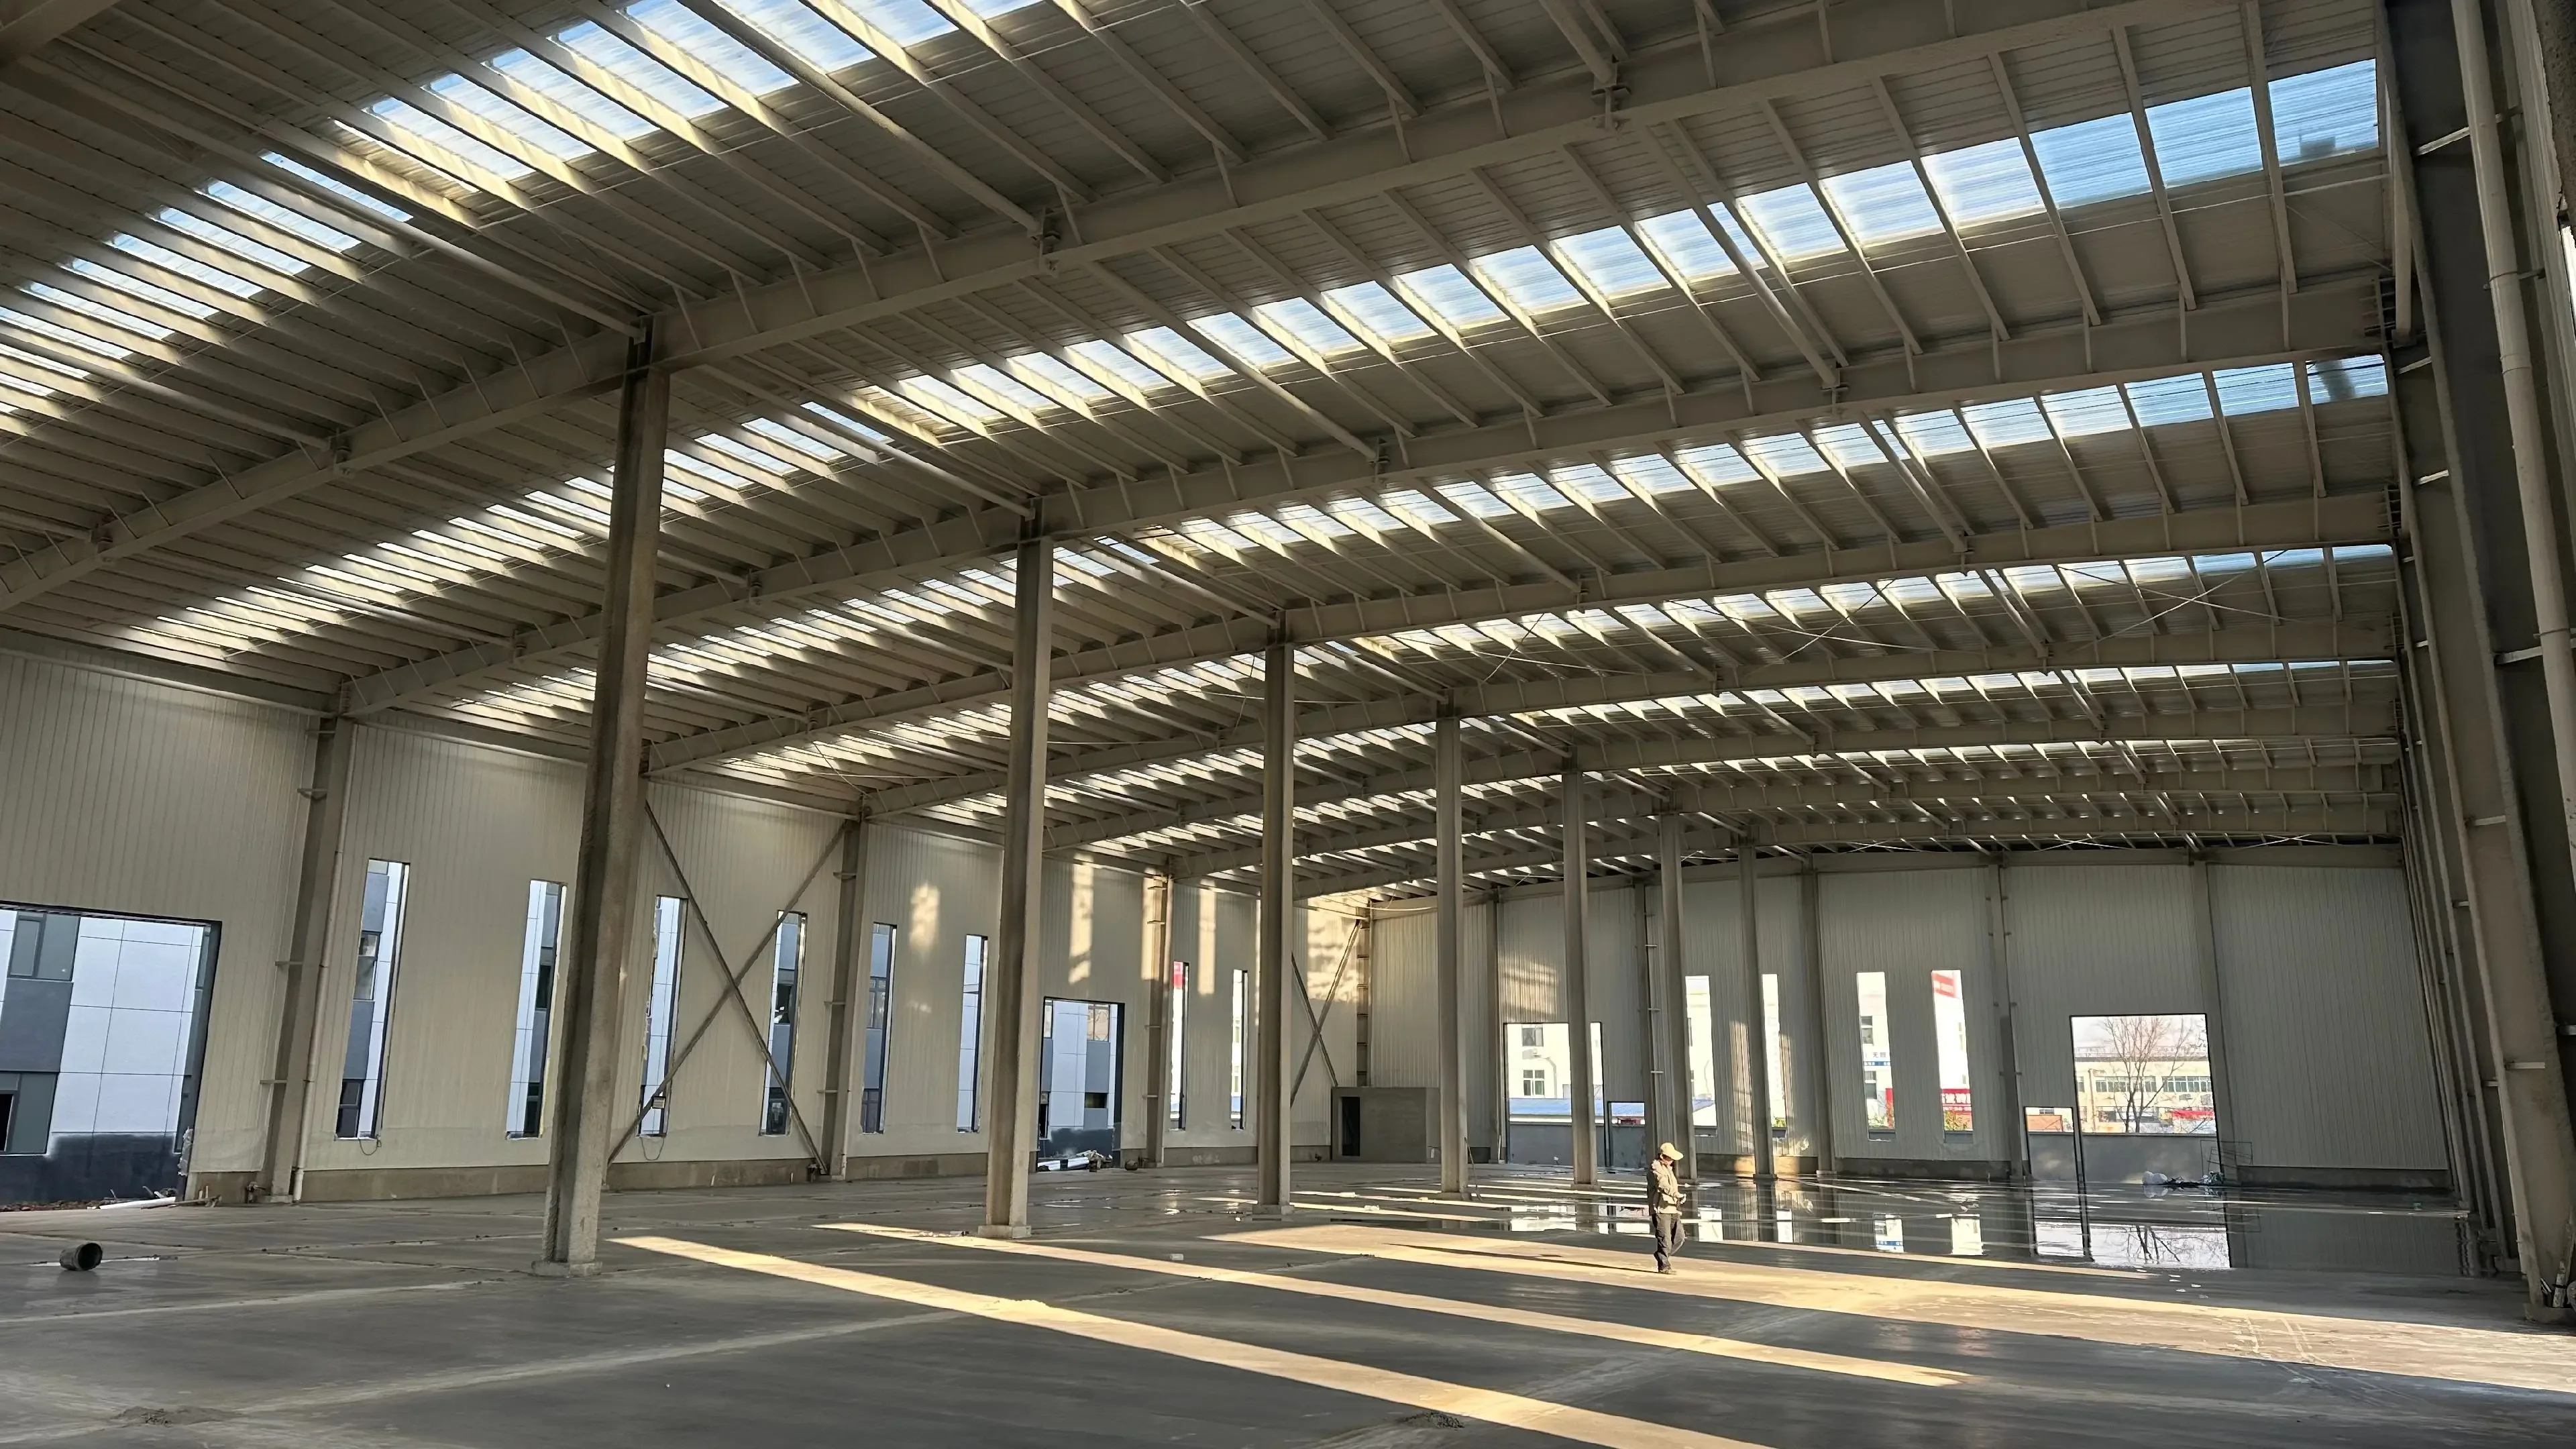
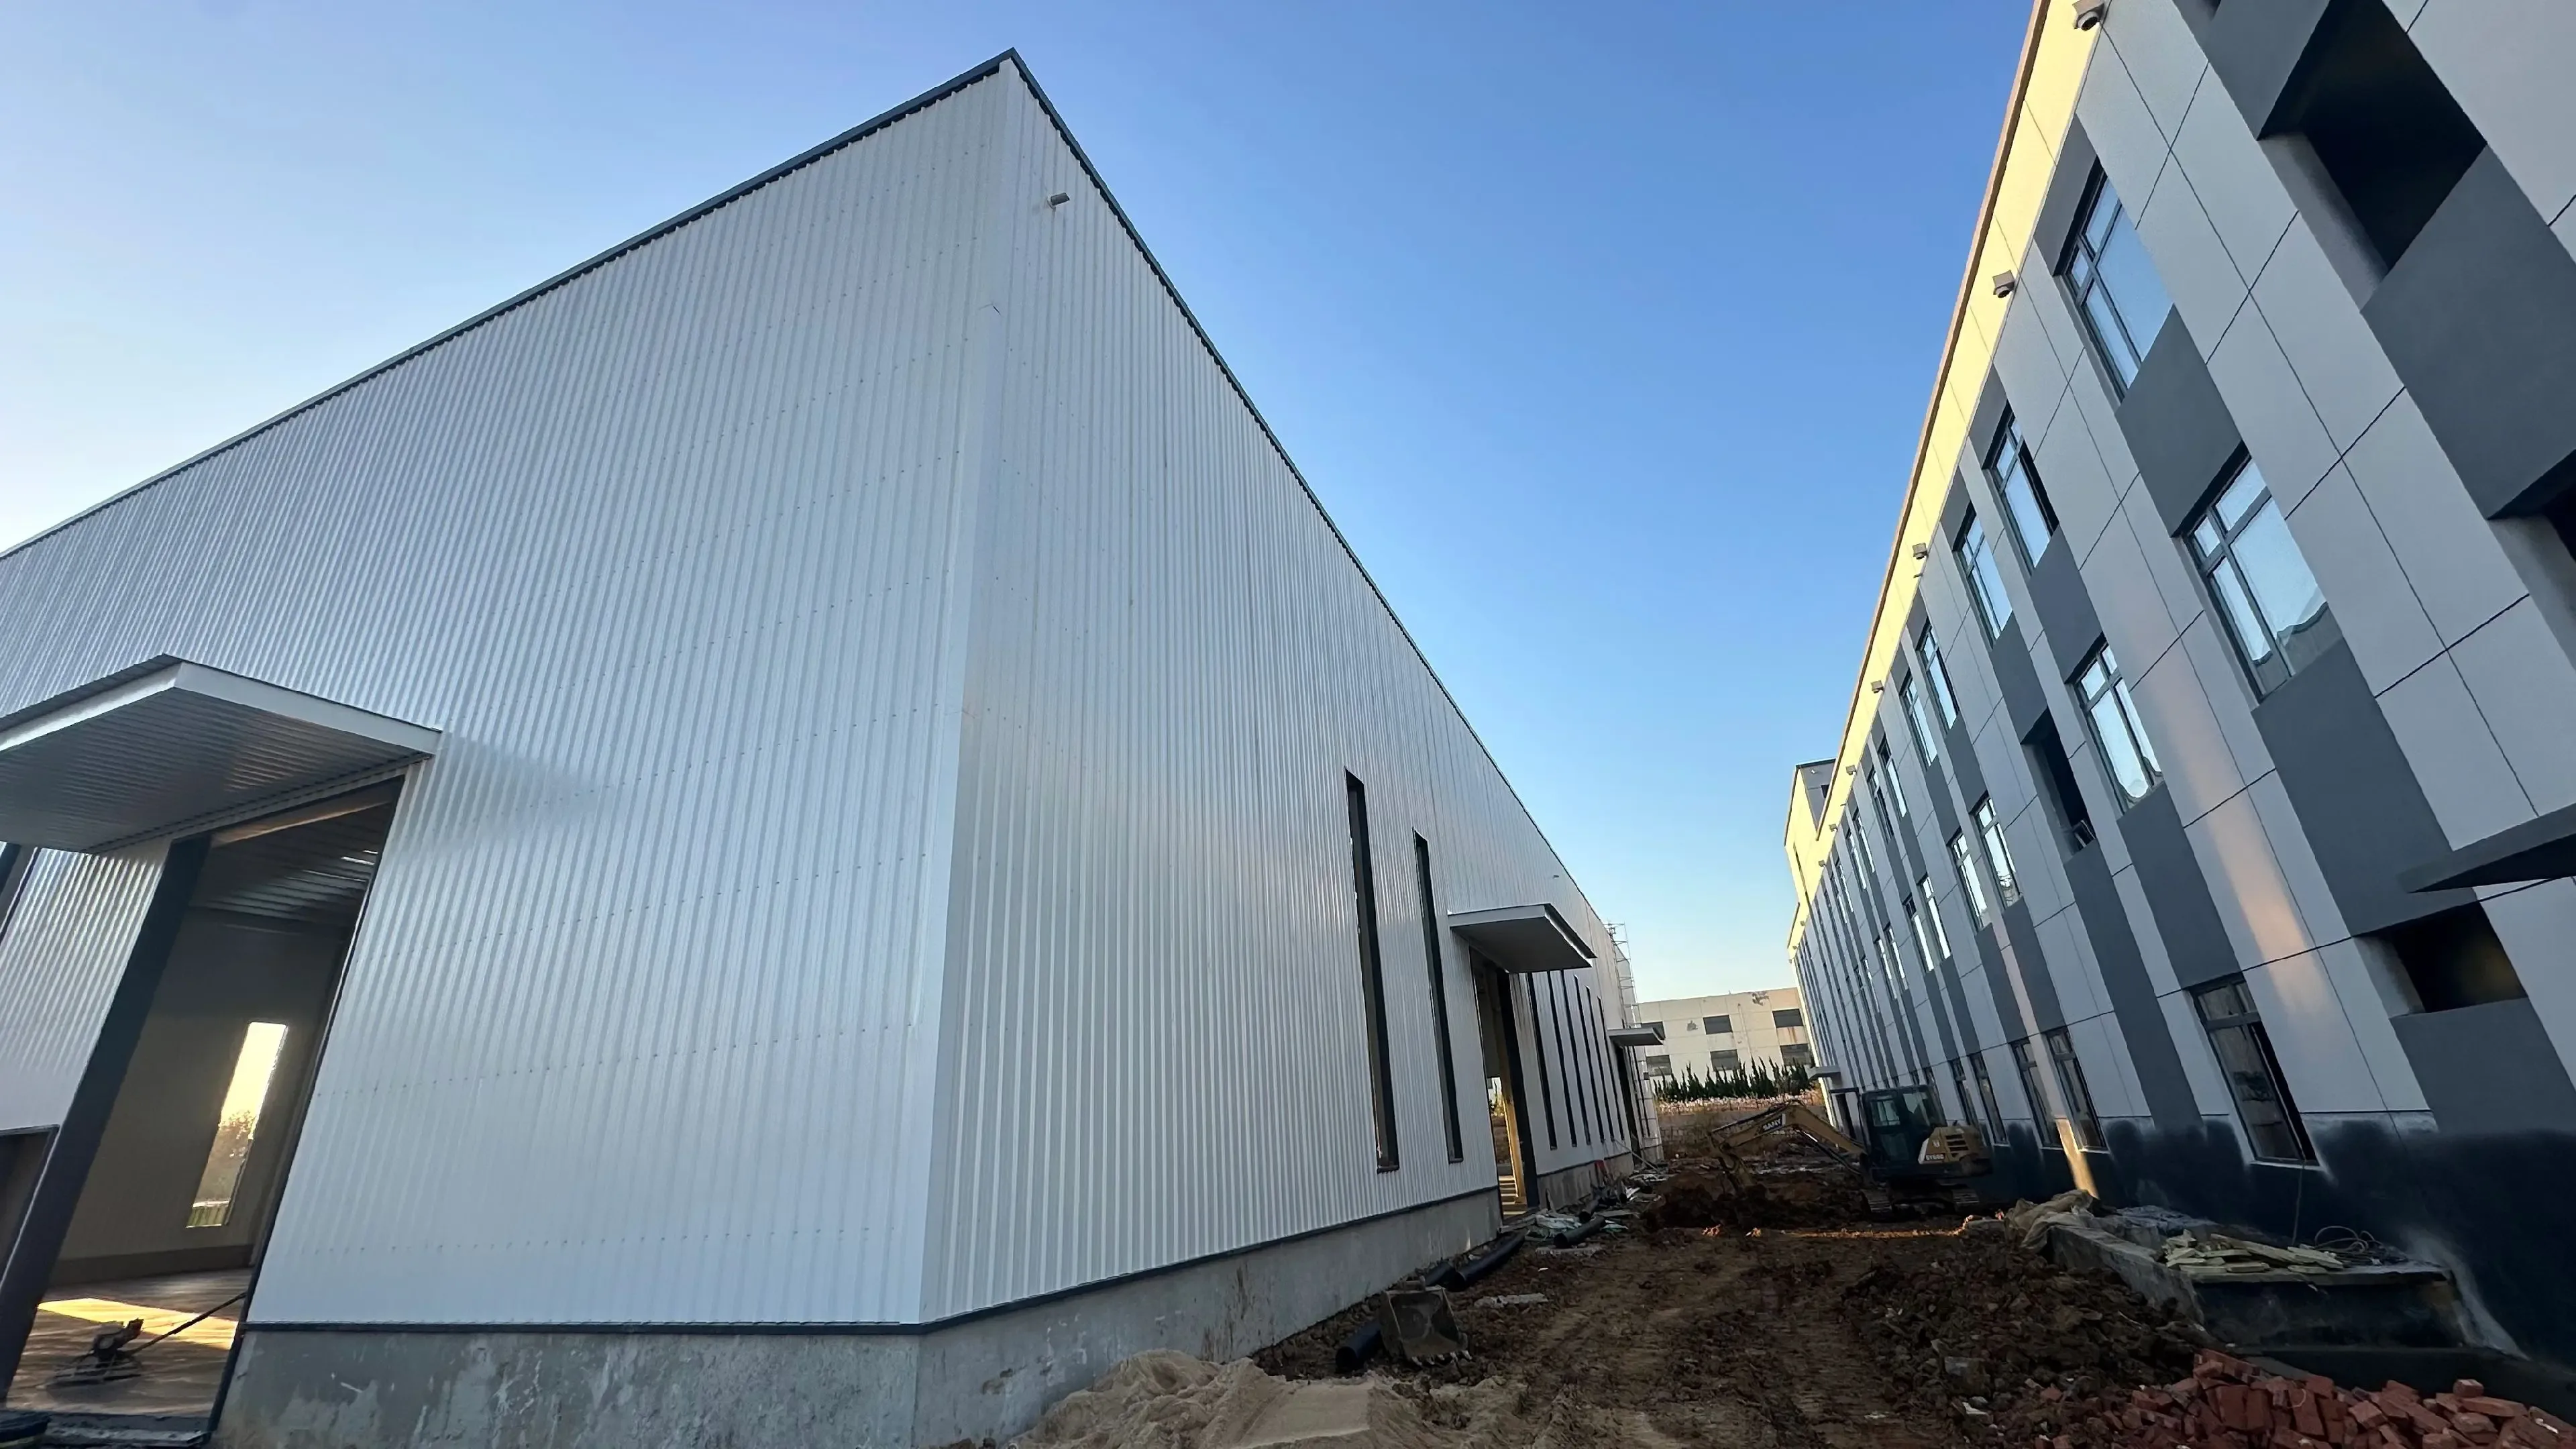
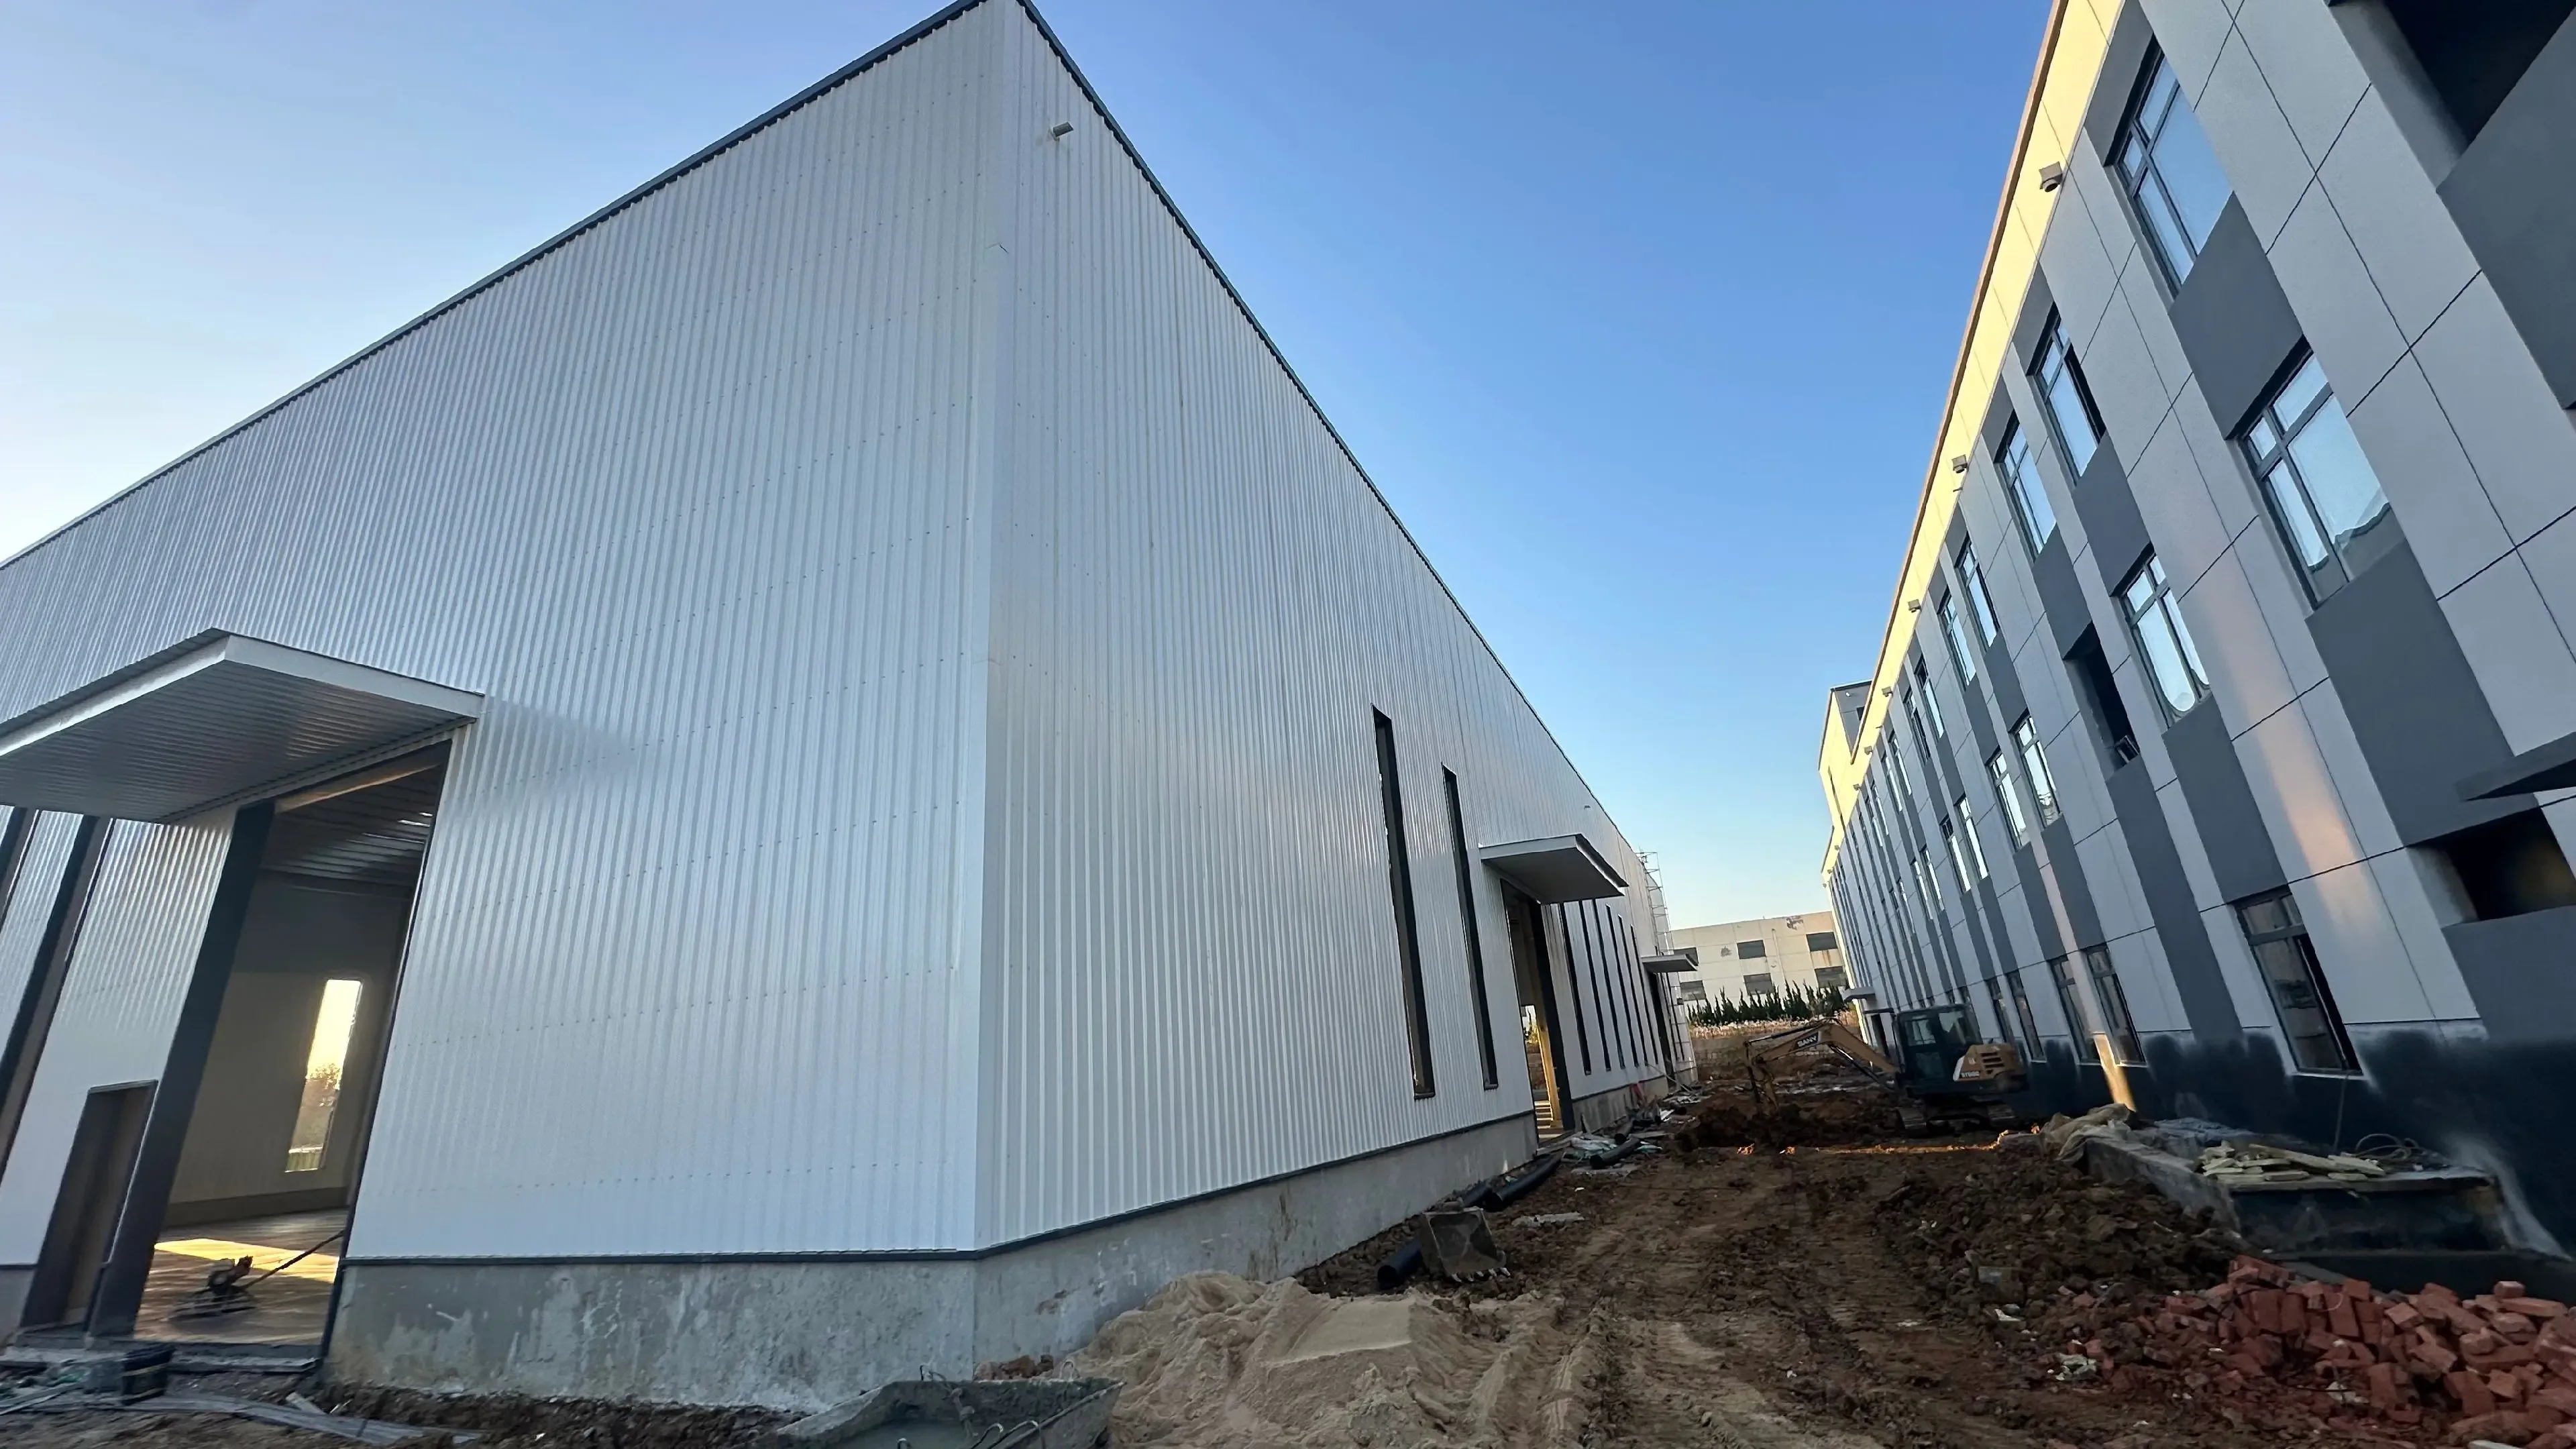
This case covers an 1,800 m² Prefabricated Steel Structure Warehouse using a portal-frame structural concept. For an industrial or logistics facility, the delivery objective is broader than supplying steel tonnage: the frame, secondary members, roof and wall envelope, openings, foundations and erection sequence must work as one coordinated system.
A well-managed package gives the owner usable storage volume and maintainable building fabric; gives the EPC contractor defined supply boundaries and interfaces; and gives the engineer a traceable route from design assumptions to fabrication drawings, inspection records and site installation information. The final configuration must follow the project brief and the approved design documents rather than generic warehouse assumptions.
Engineering Documentation & Quality Assurance
Reliable project delivery depends on traceable engineering documentation and clearly defined quality-control procedures. Depending on the agreed project scope, the documentation package may include approved fabrication drawings, material traceability records, inspection reports, protective coating records, packing lists and handover documentation.
02 · Design Basis and Engineering Coordination
The structural solution should be developed against an agreed Design Basis. Before design release, the owner/EPC team and the responsible Australian design professionals should coordinate the intended building use, dimensions, site conditions, applicable code pathway, loads, serviceability limits, durability requirements and approval responsibilities.
| Design input / interface | Why it matters | Evidence to align |
|---|---|---|
| Building geometry and use | Sets grids, clearances, access and operational requirements. | Approved architectural drawings; design brief; opening and equipment schedules. |
| Site actions and design criteria | Influences frame members, bracing, connections and serviceability. | Site-specific design criteria and signed engineering calculations/drawings. |
| Foundations and hold-downs | Transfers reactions into civil works and controls fit-up risk. | Column reactions, base-plate details, anchor-bolt plan and survey tolerances. |
| Envelope and penetrations | Coordinates purlins, girts, cladding, doors, vents and flashings. | Cladding layouts, interface details, approved openings and supplier data. |
For EPC delivery, the most valuable engineering output is a coordinated revision set: design criteria, general arrangement, member and connection details, anchor-bolt setting-out information, cladding interfaces and a controlled record of design changes. Any project-specific crane loads, mezzanines, suspended services, solar panels or future expansion requirements should be declared early rather than added after fabrication.
03 · Fabrication Planning and Quality Control
A reliable steel package connects the approved design to identifiable physical components. The control chain should link drawing revision, material identification, cutting and drilling, fit-up, welding, dimensional inspection, surface preparation, coating, packing and shipment. The exact inspection and test plan (ITP) is agreed for the contract and should define inspection stages, acceptance criteria, responsibilities and record retention.
Before fabrication
- Approved shop drawings and revision control
- Material list and heat/batch traceability where required
- Welding and inspection requirements agreed in the ITP
- Connection, bolt and erection-marking coordination
During and after fabrication
- Fit-up and dimensional inspection records
- Welding/NDT records where specified by the project
- Non-conformance, corrective action and re-inspection trail
- Piece marks, packing lists and dispatch reconciliation
These records enable an EPC contractor or engineer to trace an installed member back to the relevant drawing and inspection history. Acceptance standards, NDT extent and required certificates must be set by the contract documents and applicable design/quality requirements; they should not be inferred from a photograph alone.
04 · Corrosion Protection and Coating Evidence
The source case description lists Sa 2.5 abrasive blast cleaning, an epoxy zinc-rich primer and polyurethane topcoats. Suitability depends on the actual atmospheric corrosivity, exposure category, design life, maintenance plan, transport conditions and coating manufacturer's requirements. These details should be confirmed in the project coating specification before production.
Coating quality record set
Paint names alone do not prove durability. The acceptance record should show the specified preparation grade, coating products, required dry-film thicknesses, inspection results and treatment of damaged areas. The final system and target values must be taken from the approved project specification, not assumed from this case summary.
05 · Roof, Wall and Fire-Performance Interfaces
The original case description refers to fire-retardant sandwich panels for the roof and wall envelope. For an Australian project, the required fire, thermal, condensation, weatherproofing and building-class performance must be established by the project design team. A general product description is not the same as evidence of a tested fire-resistance level or code compliance.
Coordination should cover panel type and thickness, support spacing, fastener selection, side/end laps, ridge and eave details, flashings, gutters and downpipes, door and louvre openings, penetrations, insulation continuity and interfaces with fire compartments. Product certificates, test classifications and installation details should be submitted where required by the approval pathway and contract.
06 · Shipping, Site Interfaces and Erection Readiness
Fabrication quality can be undermined by unclear package boundaries or incomplete site information. The handover from factory to site should therefore connect each shipment to erection drawings, piece marks, packing lists, bolt schedules and the agreed erection sequence. Packing, lifting and transport protection should be planned around member dimensions, coating sensitivity, unloading equipment and site storage conditions.
| Interface risk | Recommended control | Record / check |
|---|---|---|
| Anchor bolts or foundations out of tolerance | Coordinate setting-out data and site survey before steel erection. | Approved bolt plan; survey results; discrepancy resolution. |
| Missing or mismatched components | Use piece-marked packages and reconcile each dispatch. | Packing list; loading list; receipt inspection. |
| Coating damage in transit or on site | Specify lifting, dunnage, storage and repair methods. | Arrival condition report; repair and re-inspection log. |
| Unclear erection sequence or temporary stability | Agree sequence, temporary bracing and contractor responsibilities. | Erection method statement and relevant lift plans. |
07 · The Engineering Handover Evidence Pack
The practical proof of competence is a controlled package of records that allows reviewers to establish what was specified, what was fabricated, what was inspected and what was shipped. The final submittal index should be tailored to the purchase order, inspection plan and local approval requirements.
| Evidence item | Question it answers | Primary reviewer |
|---|---|---|
| Design basis and approved drawings | Was the package designed to the agreed brief and revision? | Engineer / EPC |
| Material certificates and traceability records | Can supplied steel be matched to the specified material? | Engineer / QA-QC |
| Welding, dimensional and NDT records as specified | Were the defined fabrication checks completed and accepted? | EPC / inspector |
| Surface preparation and coating reports | Does the recorded finish meet the approved coating specification? | Owner / QA-QC |
| Packing, dispatch and component lists | Can the shipment be checked and erected without ambiguity? | Logistics / site team |
| Deviations, repairs and close-out records | Were issues documented, resolved and re-checked? | EPC / owner / engineer |
08 · Value for EPC Contractors, Engineers and Owners
For overseas EPC contractors
Clear package boundaries, revision control, interface schedules and dispatch records help reduce scope gaps between the steel supplier, local civil contractor, erector and envelope trades. The project team can map each deliverable to the purchase order and master schedule.
For consulting and structural engineers
A defined design-basis workflow and traceable fabrication records support design review, technical queries, inspection planning and resolution of deviations. The responsible local engineer retains authority over project-specific design assumptions and statutory approvals.
For owners and asset managers
Material, coating, product and handover records make it easier to assess maintainability, plan future repairs and retain the technical history of the building. Fire and performance claims should be supported by the relevant project and product documents.
Moving from a reference case to a project-specific solution? Review our Prefabricated Steel Structure Warehouse solutions to explore the warehouse package and then define the required dimensions, structural criteria, envelope, interfaces and supply boundaries for your project.
09 · Scope and Verification Note
The case facts published here are limited to the 1,800 m² area, portal-frame form, Q355B steel reference, the stated blast-cleaning and paint-system description, and the stated sandwich-panel envelope. This page does not publish member sizes, load values, design calculations, project-specific code clauses, fire-resistance ratings, coating thickness targets, certificates, inspection results, delivery dates or client acceptance records. Those items must be confirmed from the project document register before being represented as verified outcomes.
For a live tender or project review, use this page as a discussion framework and request the relevant controlled documents under the applicable confidentiality and disclosure arrangements. This keeps the technical review transparent and allows the EPC, engineer and owner to evaluate evidence against their own acceptance criteria.